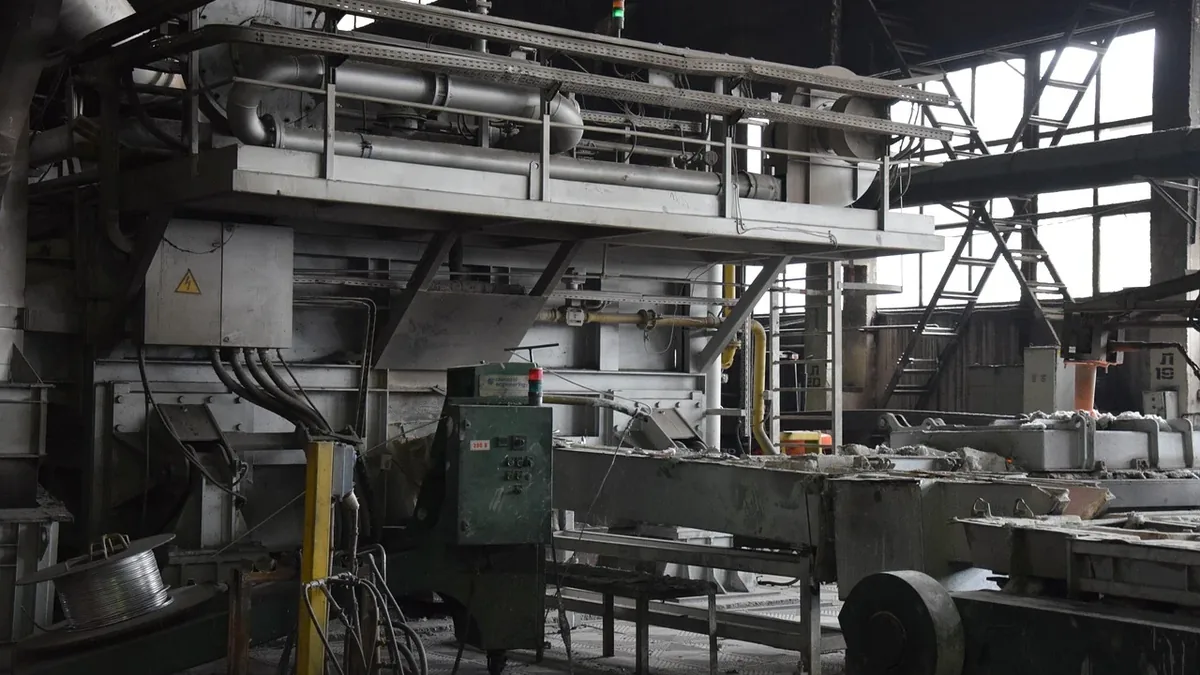
Data Historians And Analytics
| Primary function | Collect and store time-series process data from industrial equipment |
|---|---|
| Data input | Sensor readings, controller tags, and alarm events from the factory floor |
| Data storage | High-speed, compressed, time-series database |
| Typical deployment | On-premises server or virtual machine within the plant network |
| Key analytical capability | Trend analysis, performance calculation, and event replay |
| Original use | Long-term archival and retrieval of operational data for manufacturing industries |
| Integration | Connects to PLCs, SCADA systems, and higher-level analytics platforms |
Origin and history
The conceptual and technological foundations for data historians emerged from the industrial sectors of the United States and Western Europe in the late 1970s and early 1980s. This development was driven by the need to capture and store vast amounts of time-series data from plant floor sensors and control systems, which traditional databases could not handle efficiently. Early systems were often proprietary, hardware-centric solutions provided by major automation vendors to work specifically with their own programmable logic controllers (PLCs) and distributed control systems (DCS). The term "historian" itself became standardized in the 1990s as these systems evolved into dedicated software applications focused on high-speed data compression and retrieval. The integration of analytics capabilities is a more recent evolution, accelerating in the 2000s with the rise of greater computing power and advanced statistical software. This convergence has transformed the historian from a passive recording device into an active platform for process intelligence.
What it is for
A data historian's primary function is to collect, compress, and store time-series process data from equipment and instruments on the factory floor at very high speeds. It serves as the single, reliable source of truth for all operational data, preserving a detailed record of temperatures, pressures, flows, valve positions, and motor states over years or decades. This stored history is essential for regulatory compliance, forensic analysis of process upsets or product quality deviations, and generating performance reports. The analytics layer built upon this data is used to identify inefficiencies, predict equipment failures through pattern recognition, and optimize production recipes and energy consumption. Ultimately, the combined system informs capital investment decisions by providing quantifiable evidence of process bottlenecks or reliability issues. It turns raw operational data into actionable knowledge for improving safety, quality, and throughput.
Overview
A data historian and analytics system is a specialized software infrastructure that sits between the operational technology (OT) network of the factory and the information technology (IT) systems of the enterprise. At its core is a time-series database engine that uses compression algorithms to efficiently store billions of data points with precise timestamps. It connects to controllers and sensors via industrial protocols like OPC to collect data in real-time, often at sub-second intervals. The analytics component encompasses tools ranging from basic dashboarding and trend visualization to advanced applications like statistical process control, machine learning models, and digital twin simulations. This system typically feeds summarized information into manufacturing execution systems (MES) and enterprise resource planning (ERP) software. Its implementation represents a significant technical project involving IT/OT integration, data modeling, and the development of use cases to deliver specific business value.
What to know
Implementing a data historian is not merely a software installation but a foundational project that requires careful planning around data granularity, retention policies, and tag structure. The initial and ongoing cost is not trivial, encompassing software licenses, dedicated server hardware, engineering hours for configuration, and continuous maintenance. Data quality is a critical challenge; the system will only be as useful as the accuracy and reliability of the underlying sensors and the correctness of the data tags, making a comprehensive commissioning process essential. Security is paramount, as the historian becomes a critical asset requiring robust protection from cyber threats while enabling necessary access for engineers and analysts. The analytics piece demands specific skill sets, often requiring process engineers to collaborate with data scientists to build meaningful models that reflect physical realities. Success depends on clear ownership and governance, ensuring the system is used proactively rather than just as a digital logbook for post-incident investigation.
Common questions
What is the difference between a data historian and a traditional relational database? A historian is optimized for writing and reading sequential time-stamped data from many sources simultaneously, while a relational database is better for transactional data and complex queries across related tables. How long is data typically retained? Retention policies vary, with high-frequency raw data often kept for 1-3 years online, and then summarized or archived for longer-term compliance, sometimes for decades. Can it connect to equipment from different manufacturers? Yes, modern historians use standard industrial communication protocols to aggregate data from a heterogeneous mix of PLCs, DCS, and smart devices across the plant. What is a "tag"? A tag is the unique identifier for a single data source, such as "Tank_101_Temperature," and a system can contain tens or hundreds of thousands of tags. Is cloud deployment feasible? While on-premise is traditional, cloud-based historians are now an option, though considerations around data latency, bandwidth, and security require thorough evaluation. Who within the organization uses the system? Users range from control room operators and maintenance technicians viewing real-time trends, to process engineers analyzing performance, and plant managers reviewing overall equipment effectiveness (OEE) dashboards.
Pros and cons
A primary advantage is the creation of an immutable, detailed record of plant operations, enabling deep forensic analysis and supporting consistent, data-driven decision-making. The system can significantly reduce time spent manually collecting data and generating reports, freeing engineering resources for higher-value tasks. Effective analytics can lead to substantial cost savings through predictive maintenance, yield improvement, and energy optimization. However, a major con is the risk of creating a costly "data graveyard" if the implementation lacks clear business objectives and operational buy-in, where data is collected but never meaningfully analyzed. The complexity of integration can lead to prolonged projects that exceed budgets and fail to deliver promised returns, particularly if underlying data quality is poor. A common mistake is underestimating the ongoing internal resource requirement for tag management, model maintenance, and user support, leading to system stagnation. Organizations sometimes regret the investment when they treat it as a purely IT project without the active, sustained involvement of process and production experts who understand the data's context.
Who it suits
This technology suits capital-intensive process industries with continuous or batch production, such as oil and gas, chemicals, pharmaceuticals, power generation, and metals manufacturing, where process variability directly impacts cost and quality. It is particularly valuable for organizations with existing automation infrastructure that are seeking to move from reactive to proactive operations and require robust data for regulatory reporting and quality audits. Facilities experiencing frequent unexplained process upsets or product quality issues, where root cause analysis is hindered by a lack of historical data, are strong candidates. The investment is best justified for companies with the technical personnel to steward the system, including control engineers, data analysts, and IT specialists capable of supporting the operational technology environment. It is less suited to very small, low-margin operations with simple processes, manual data collection, and limited technical staff, where the complexity and cost may outweigh the potential benefits.
Latest Data Historians And Analytics news
Latest reporting
U.S. Manufacturing Output Dips in August Amid Major Factory
Federal Reserve data shows a 0.3% drop in manufacturing output for August, breaking a seven-month growth streak.
Vention opens Montreal lab to train AI with factory data
Vention has opened a Physical AI Lab in Montreal to develop robotic manipulation models using data from hundreds of robot cells it deploys annually.
NAM's Timmons: AI and Tax Policy Drive Manufacturing Growth
NAM President Jay Timmons says the 2025 tax law and AI-driven data center demand are fueling a surge in U.S. Manufacturing activity across many...
Chef Robotics CEO to Discuss Food AI at RoboBusiness
Chef Robotics CEO Rajat Bhageria will argue food is the hardest challenge for physical AI at RoboBusiness 2026, citing data from over 118 million...